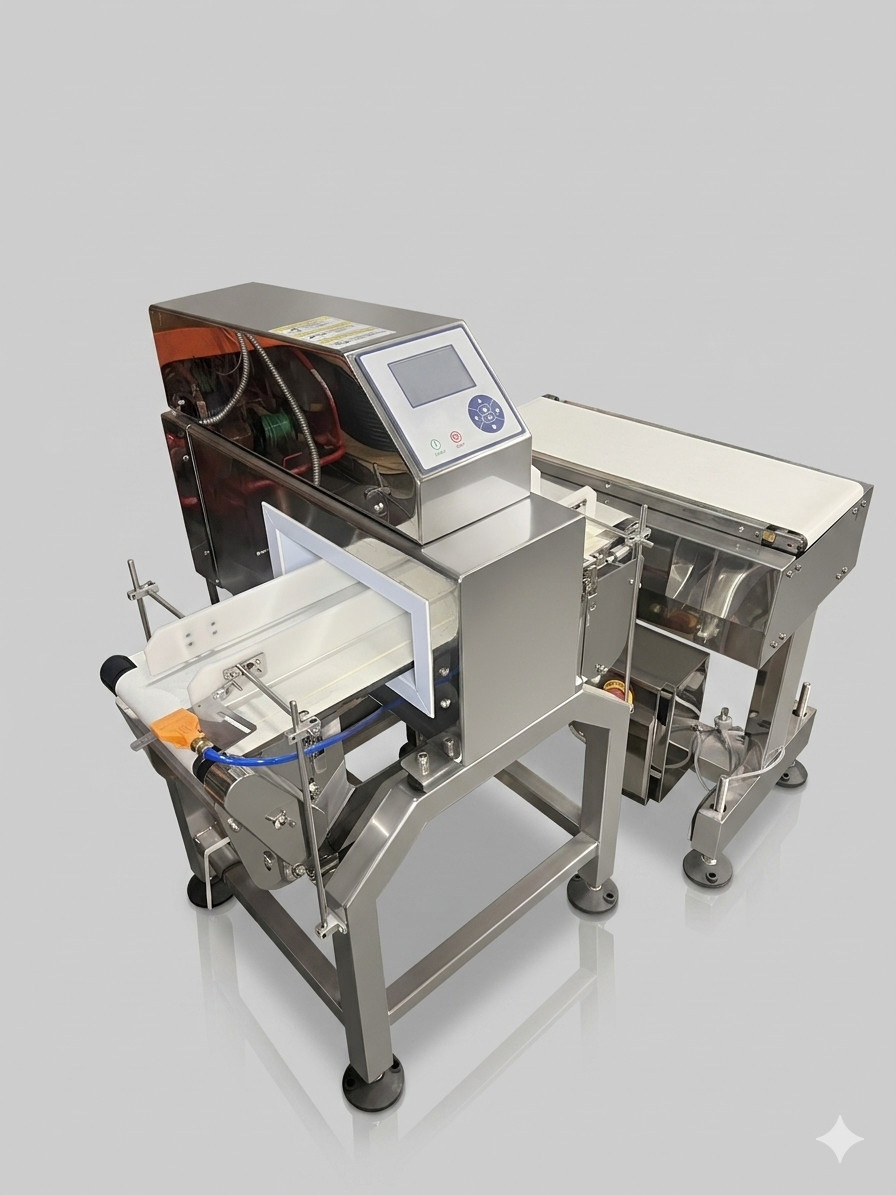
When you are adding product inspection checkweighing to a food processing line, the central question is whether a given unit can keep up with your packaging flow while catching the contaminants that matter. The Industrial Food Metal Detector Machine with Conveyor Belt for Food Safety, listed at USD 2,850.00, is one option that bundles the detector head and conveyor into a single inspection station. But is it the right fit for your operation? Let's walk through what this unit offers and where you should pause.
Quick Verdict
If you need a ready-to-integrate metal detection setup with a conveyor already attached, this used machine deserves a close look. Its design targets high-throughput food lines that handle flexible or challenging packaging, and the integrated detector head is built to spot ferrous and stainless steel contaminants as products move through. The USD 2,850.00 price places it as a mid-cost investment for a specialized piece of inspection equipment. It is not a portable handheld scanner; this is a fixed station meant to become part of a larger production flow.
Who It Suits
This unit suits food manufacturers that run continuous packaging lines and need inline metal detection without building a custom rig. The dual-lane integration means the primary inspection unit transfers products to a secondary conveyor for further distribution, so it fits operations already using multi-lane layouts. It is also a reasonable match for facilities that process flexible or hard-to-inspect packages, since the system is described as specifically designed to stabilize and inspect those formats. If your line handles rigid trays or bulky cartons, the rectangular aperture might still work, but you will want to think about product height and width.
What Stands Out from the Listed Details
The most notable feature is the integrated metal detector head with a rectangular aperture. This is not a separate component that you have to align yourself; it is built into the conveyor station, which simplifies installation. The high-sensitivity search coil is designed to identify sub-millimeter metal particles, including ferrous and stainless steel fragments. That level of detection is important for protecting both consumers and your brand reputation.
The intuitive color touchscreen control is another practical touch. It gives operators a straightforward interface for setting parameters and monitoring the inspection process. On a busy production floor, a clear control panel reduces training time and the risk of operator error.
The dual-lane integration is a differentiator as well. Because the primary inspection unit directly transfers to a secondary conveyor, you can place this machine upstream of a distribution point or connect it to an existing multi-lane line. That flexibility could save you from purchasing additional conveying equipment.
Meaningful Trade-Offs
This is a used unit, and its condition is listed as "Used" without further detail. That means you should carefully evaluate the wear on the conveyor belt, the detector coil, and the touchscreen before committing. Used industrial equipment can be a smart way to control costs, but it can also bring hidden maintenance needs.
The price of USD 2,850.00 reflects the integrated nature of this station. For a small operation, that is a significant capital outlay. If you only run occasional batches, a simpler or smaller unit might be more practical. Also, the description focuses on metal detection; it does not mention checkweighing capabilities. If you need weight verification alongside contaminant detection, this system alone may not cover that requirement.
Bottom Line
The Industrial Food Metal Detector Machine with Conveyor Belt for Food Safety is a solid candidate for established food packaging lines that need reliable inline metal detection with conveyor transport already included. Its dual-lane capability and high-sensitivity search coil make it particularly attractive for high-throughput operations handling flexible packaging. Just go in with your eyes open about the used condition and confirm that the aperture size and conveyor dimensions match your actual product flow. If they do, this unit could become a dependable part of your food safety inspection setup.